CCMT09T302/04/08 Carbide Turning Inserts: Applications & Selection Tips
Author : Surya makeyoueasy | Published On : 08 Oct 2026
Introduction
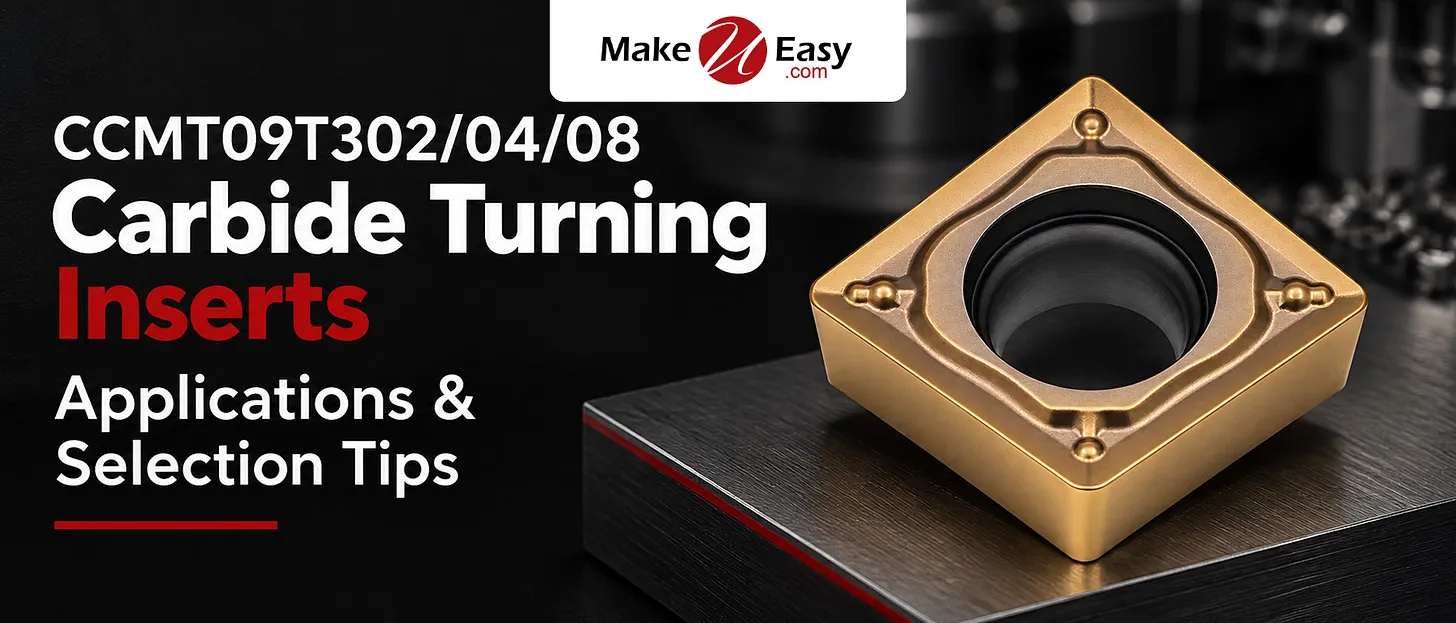
CCMT09T302, CCMT09T304, and CCMT09T308 are positive carbide turning inserts commonly used for CNC turning, boring, facing, profiling, and finishing. Their 80° diamond geometry and 7° clearance angle provide a useful combination of cutting access and reduced cutting forces. The main difference between these three variants is the nose radius, making selection important for achieving the required surface finish, edge strength, and machining stability.
What Are CCMT09T302/04/08 Inserts?
CCMT is an ISO insert designation for a positive 80° diamond-shaped turning insert with a 7° clearance angle. The 09T3 size corresponds to an inscribed circle of approximately 9.525 mm, while the final digits identify the nose radius.
These inserts are widely used in compatible CNC turning holders for general turning and profile machining. Depending on the grade and chipbreaker, CCMT inserts can be selected for steel, stainless steel, cast iron, and other workpiece materials.
CCMT09T302/04/08 Specifications
SpecificationCCMT09T302CCMT09T304CCMT09T308Insert Shape80° Diamond80° Diamond80° DiamondClearance Angle7°7°7°IC9.525 mm9.525 mm9.525 mmThickness*3.18–3.97 mm3.97 mm3.97 mmHole Diameter*4.4 mm4.4 mm4.4 mmNose Radius0.2 mm0.4 mm0.8 mmTypePositivePositivePositiveTypical UseFine finishing/profilingFinishing/general turningGeneral turning/finishing
*Dimensions can vary by exact manufacturer and insert construction, so verify the product catalogue before ordering. Tungaloy’s catalogue lists CCMT09T302, 304 and 308 with 0.2, 0.4 and 0.8 mm radii respectively, while product listings confirm the 9.525 mm IC for the CCMT09T3 family.
Understanding the CCMT Code
The designation can be read as follows:
-
C: 80° diamond-shaped insert
-
C: 7° clearance angle
-
M: Tolerance class
-
T: Insert style with hole
-
09: Insert size
-
T3: Thickness/style designation
-
02: 0.2 mm nose radius
-
04: 0.4 mm nose radius
-
08: 0.8 mm nose radius
The exact complete designation can include additional letters for chipbreaker, grade, coating, or manufacturer-specific geometry.
CCMT09T302 vs. CCMT09T304 vs. CCMT09T308
CCMT09T302: 0.2 mm Nose Radius
The 0.2 mm radius is useful when a smaller cutting radius is preferred for fine finishing, detailed profiling, or machining smaller features. It can help reduce cutting forces, but the smaller edge radius generally requires a stable setup and appropriate cutting conditions.
CCMT09T304: 0.4 mm Nose Radius
The 0.4 mm radius is a versatile choice for finishing and general turning. It provides a practical balance between surface finish, cutting forces, and edge strength.
CCMT09T308: 0.8 mm Nose Radius
The 0.8 mm radius provides a larger cutting edge and can offer greater edge strength. It is commonly selected for general turning and finishing when the machine and workpiece provide sufficient rigidity.
Important: A larger nose radius does not automatically produce a better surface finish. Feed rate, cutting speed, tool stability, workpiece material, and insert geometry all influence the final result.
Main Applications of CCMT Inserts
1. External Turning
CCMT inserts are commonly used for machining shafts, cylindrical surfaces, steps, and other external features.
2. Internal Boring
Compatible CCMT boring tools can be used for internal diameters where the insert has sufficient clearance and the boring setup is rigid.
3. Profile Turning
The 80° diamond shape provides useful access for profile turning and machining component contours.
4. Finishing
Positive geometry and smaller nose-radius options make CCMT inserts suitable for finishing applications when the correct grade, chipbreaker, and cutting parameters are selected.
5. Stainless Steel Machining
CCMT inserts are available with grades and chipbreakers specifically intended for stainless steel. For example, Iscar lists CCMT09T304-SM IC807 for steel, stainless steel, cast iron, hard materials, and superalloys/titanium, with a recommended application range that includes external and internal turning.
How to Select the Right CCMT Insert
Consider these factors before choosing a CCMT09T3 insert:
Workpiece Material
Select the carbide grade and chipbreaker according to whether you are machining steel, stainless steel, cast iron, aluminium, or another material.
Nose Radius
Choose 0.2 mm for finer features and low cutting loads, 0.4 mm for a balanced general-purpose option, or 0.8 mm when greater edge strength and suitable rigidity are required.
Cutting Depth and Feed
Match the insert geometry to the intended depth of cut and feed rate. Manufacturer data should be the primary reference for cutting conditions.
Machine and Tool Rigidity
A rigid machine, holder, workpiece, and tool setup helps the insert perform consistently. Reduce tool overhang where possible.
Holder Compatibility
Verify the insert size, screw/clamping arrangement, and tool-holder designation before purchasing. CCMT09T3 inserts are used with compatible turning and boring holders.
Common Selection Mistakes
-
Choosing the grade without considering the workpiece material
-
Using a large nose radius on a low-rigidity setup
-
Selecting an insert only by price
-
Ignoring the chipbreaker design
-
Using cutting parameters from an unrelated grade
-
Failing to verify holder and insert compatibility
-
Continuing to machine with a chipped or heavily worn edge
Why Choose MakeYouEasy?
MakeYouEasy provides CNC turning inserts, cutting tools, tool holders, milling tools, and machining accessories for manufacturing applications.
For CCMT inserts, selecting the right nose radius, grade, chipbreaker, and compatible holder can help achieve more consistent machining performance and surface quality.
Conclusion
CCMT09T302, CCMT09T304, and CCMT09T308 share the same CCMT09T3 family geometry but differ mainly in nose radius. The 0.2 mm radius suits fine and detailed work, 0.4 mm provides a versatile balance, while 0.8 mm offers a stronger cutting edge for suitable general turning applications.
For the best results, select the grade and chipbreaker according to the workpiece material, verify holder compatibility, and follow the manufacturer’s recommended cutting conditions.
Frequently Asked Questions
1. What is the difference between CCMT09T302 and CCMT09T304?
CCMT09T302 has a 0.2 mm nose radius, while CCMT09T304 has a 0.4 mm nose radius.
2. What is the difference between CCMT09T304 and CCMT09T308?
CCMT09T304 has a 0.4 mm radius, while CCMT09T308 has a 0.8 mm radius.
3. Can CCMT09T3 inserts be used for stainless steel?
Yes, select a grade and chipbreaker specifically recommended for the stainless steel being machined.
4. What is CCMT09T3 mainly used for?
It is commonly used for external turning, internal boring, profiling, facing, and finishing.
5. How do I choose the correct CCMT nose radius?
Choose according to the required finish, feature size, cutting conditions, and machine and workpiece rigidity.
Popular Search Keywords
CCMT09T302 carbide insert, CCMT09T304 carbide insert, CCMT09T308 carbide insert, CCMT09T3 turning insert, CCMT carbide turning inserts, CCMT09T302 applications, CCMT09T304 applications, CCMT09T308 applications, 0.2 mm nose radius insert, 0.4 mm nose radius insert, 0.8 mm nose radius insert, CNC turning inserts, carbide inserts for CNC lathe
