2-Piece Can Production Line: Factory Acceptance Checks
Author : wei yi | Published On : 04 Nov 2026
A forming press’s top speed says little about saleable output from a complete line. Audit trimming, inspection and conveyors as part of the 2-piece can production line specification.
Start with the can, not the press
Define target can diameter, height, metal and annual production mix before specifying equipment. Two-piece and three-piece can processes are not interchangeable; confirm which body-forming steps the requested line actually includes.
Map the press, body forming, trimming and downstream handling as one system. Feeding, trimming, inspection and palletising can set the sustainable line rate even when a press has a higher nominal figure. Check line speed at accepted quality rather than a single maximum cycle figure. Verify tooling changeover time with the number of sizes the factory plans to run. Can diameter, height and metal thickness affect changeover tooling and scrap behaviour.
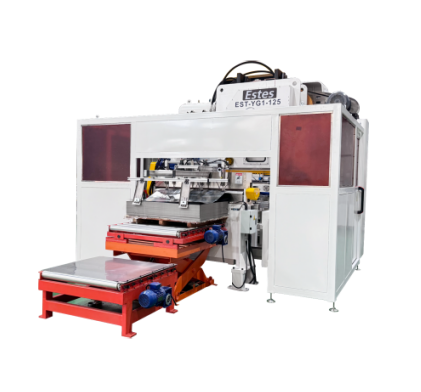
Control scrap and changeovers
Specify scrap collection, lubrication and waste handling at each forming stage. Review integration with inspection systems, conveyors and palletising equipment. Acceptance samples should include the edge and wall features that cause trouble further down the production process. Ask for a factory acceptance test using the customer's material specification.
Measure wall distribution, trim quality and dimensional consistency over a continuous run. Document which alarms and quality checks stop the line and where rejected cans are diverted.
Plan utilities, foundation loads and maintenance access before the line is shipped. Define spare tooling, technician training and restart procedures in the contract. Ask for spare tooling, operator training and maintenance access before the final equipment layout is frozen. Agree site acceptance criteria and warranty boundaries before commissioning begins.
